SPECIAL PROMOTION — Up to 40% off across many product groups, until 31 December 2026 · Click to see all promotion itemsIFM, Sensor, Automation SystemMeasuring / Testing InstrumentsTemp Indicator, Control, T/C, RTD, TimerHeater, SCR Control, Solid State, Power Supply, Control CabinetField Measuring Instruments, Pressure Gauge, Level Control, Flow MeasurementEMC, Pneumatic, Solenoid ValveInspection Test Lamp, Head Light, Automotive Measuring InstrumentWeighing Scales, Marking Machine, PrintersEducational Training SystemsHot Line Tools & Equipment SPECIAL PROMOTION — Up to 40% off across many product groups, until 31 December 2026 · Click to see all promotion itemsIFM, Sensor, Automation SystemMeasuring / Testing InstrumentsTemp Indicator, Control, T/C, RTD, TimerHeater, SCR Control, Solid State, Power Supply, Control CabinetField Measuring Instruments, Pressure Gauge, Level Control, Flow MeasurementEMC, Pneumatic, Solenoid ValveInspection Test Lamp, Head Light, Automotive Measuring InstrumentWeighing Scales, Marking Machine, PrintersEducational Training SystemsHot Line Tools & Equipment View promotion items View all
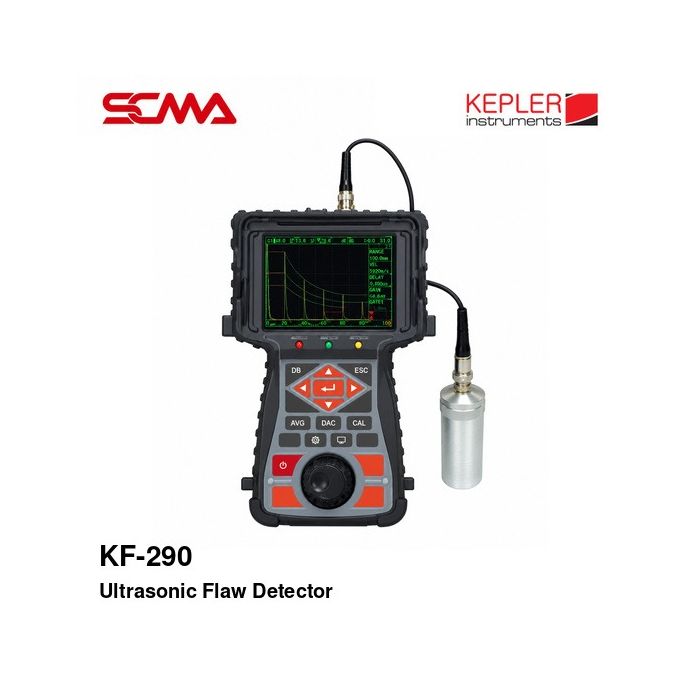
KF-290 ULTRASONIC FLAW DETECTOR KEPLER
Price on request – please contact us
Out of stock
SKU
050991
Out of stock

KF-290, KEPLER, Ultrasonic Flaw Detector, Portable Ultrasonic Flaw Detector, Digital Ultrasonic Flaw Detector, Ultrasonic Testing Equipment, UT Flaw Detector, NDT Flaw Detector, Non Destructive Testing, Ultrasonic Inspection Instrument, Weld Flaw Detector, Weld Inspection Equipment, Crack Detection Equipment, Internal Defect Detector, Metal Flaw Detection, Steel Inspection, Ultrasonic Pulse Echo Tester, Dual Probe Ultrasonic Testing, Through Transmission Testing, 0.1-15MHz Probe Frequency, 2.5-9999mm Scanning Range, 0-110dB Gain, 600-9999m/s Sound Velocity, Full Wave Rectification, RF Display, Square Wave Pulser, USB Interface, RS232 Interface, Lithium Battery, Industrial Quality Inspection, Pipeline Inspection, Pressure Vessel Inspection, Weld Quality Control, Flaw Detector, Internal Defect Detection Equipment, Ultrasonic Crack Detector, Weld Inspection Device, Steel Crack Detection Device, Non-Destructive Testing Flaw Detector, Ultrasonic Testing Instrument, Industrial Weld Inspection Tool, KEPLER Flaw Detector, KF-290 Flaw Detector, Ultrasonic Testing Tool
*Price does not include VAT
KEPLER KF-290 Ultrasonic Flaw Detector
KEPLER KF-290 Ultrasonic Flaw Detector is a portable ultrasonic flaw detector for non-destructive testing (NDT) of material defects and cracks. It is suitable for quality inspection of welds, detection of cracks, voids, and discontinuities in metal materials, as well as structural components and machinery inspections in industrial applications.
The device uses high-frequency sound wave technology to send ultrasonic signals from the probe into the workpiece and detects reflected or transmitted signals related to material discontinuities. This allows inspectors to analyze the location and characteristics of defects based on the data collected.
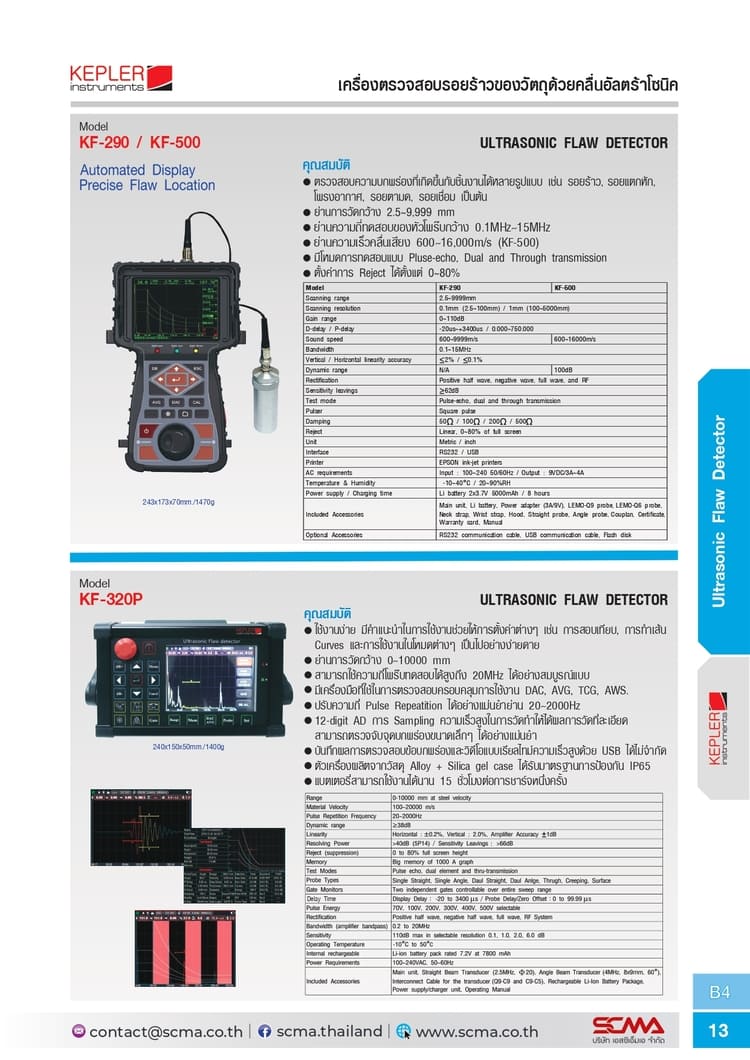
Model KF-290 supports a scanning range of 2.5-9999 mm, probe frequency from 0.1-15 MHz, and gain adjustment range of 0-110 dB. It also supports Pulse-Echo, Dual, and Through Transmission inspection modes.
The device supports signal display types including Positive Half Wave, Negative Half Wave, Full Wave, and RF. Signal delay and filtering can be adjusted according to the capabilities of the equipment to suit different inspection requirements.
KEPLER KF-290 features an RS232 and USB interface for connecting external devices as supported by the manufacturer, along with a rechargeable lithium battery system suitable for field inspections and quality control in industrial settings.
Features
- Ultrasonic flaw detector for material defect inspection
- Suitable for non-destructive testing (NDT)
- Supports weld inspection and internal material discontinuity detection
- Scanning range of 2.5-9999 mm
- Supports probe frequencies from 0.1-15 MHz
- Gain adjustment range of 0-110 dB
- Sonic velocity setting in the range of 600-9999 m/s
- Supports Pulse-Echo, Dual, and Through Transmission modes
- Supports waveform display types including Positive Half Wave, Negative Half Wave, Full Wave, and RF
- Uses a Square Pulse generator
- Damping selection available at 50, 100, 200, and 500 Ohms
- Supports Linear Reject setting range of 0-80% of the screen
- Metric or Inch measurement units selectable
- Supports RS232 and USB connectivity
Technical Specifications (Technical Specifications)
| Specifications | Details |
|---|---|
| Brand | KEPLER |
| Model | KF-290 |
| Product Type | Ultrasonic Flaw Detector |
| Testing Method | Ultrasonic Non-Destructive Testing |
| Scanning Range | 2.5-9999 mm |
| Scanning Resolution | 0.1 mm (2.5-100 mm) / 1 mm (100-5000 mm) |
| Gain Range | 0-110 dB |
| Probe Frequency / Bandwidth | 0.1-15 MHz |
| Sound Velocity Range | 600-9999 m/s |
| Vertical Linearity | <=2% |
| Horizontal Linearity | <=0.1% |
| Sensitivity Margin | >=62 dB |
| Testing Modes | Pulse-Echo / Dual / Through Transmission |
| Pulser Type | Square Pulse |
| Rectification | Positive Half Wave / Negative Half Wave / Full Wave / RF |
| Damping | 50 / 100 / 200 / 500 Ohms |
| Reject | Linear, 0-80% of Full Screen |
| Display Unit | Metric / Inch |
| Communication Interface | RS232 / USB |
| Printer Compatibility | Compatible EPSON Ink-Jet Printer (Verify Model) |
| Adapter Input | 100-240 VAC, 50/60 Hz |
| Adapter Output | 9 VDC / 3-4 A (Catalog Series Specification) |
| Battery | Rechargeable Lithium Battery |
| Battery Specification | 2 x 3.7 V, 5000 mAh (Catalog Series Listing) |
| Charging Time | Approximately 8 Hours |
| Operating Temperature | -10 to +40°C |
| Operating Humidity | 20-90% RH |
| Dimensions | 240 x 150 x 50 mm |
| Weight | Approximately 1400 g |
| Ingress Protection | Not Specified for KF-290 in Catalog |
Operation of Ultrasonic Flaw Detector
The ultrasonic flaw detector uses high-frequency sound waves to penetrate the material through a probe and couplant. When the sound wave encounters boundaries or discontinuities within the material, such as cracks, voids, or certain types of weld joints, reflections may occur back to the probe.
The device displays signal information for the inspector to analyze the position of reflected signals and the depth of indications. The results depend on the type of material, sound velocity, probe angle, surface condition of the workpiece, and calibration method.
Abnormal reflection signals do not necessarily mean a flaw in every case; therefore, signals must be evaluated according to proper inspection procedures and acceptance criteria.
Testing Modes
1. Pulse-Echo Mode
Sends ultrasonic waves into the workpiece and receives reflected signals back for inspecting internal discontinuities within the material. Suitable for weld inspections and single-sided access conditions as per inspection requirements.
2. Dual Mode
Supports separate transmission and reception of signals, requiring selection of probes and connection methods suitable for the measurement system.
3. Through Transmission Mode
Checks by sending waves through the workpiece to a receiver on the opposite side to evaluate signal changes that pass through. Proper placement of transmitter and receiver heads is required.
Signal Amplification and Processing System
Gain Adjustment: Signal amplification can be adjusted from 0-110 dB to suit the level of signals being inspected.
Rectification: Supports displaying Positive Half Wave, Negative Half Wave, Full Wave and RF signals to select the waveform characteristics according to usage.
Damping: Can choose values of 50, 100, 200 or 500 Ohms to adjust circuit operation according to probe type and testing method.
Reject: Supports setting Linear Reject in the range of 0-80% of the screen. Using Reject may cause some small signals not to be displayed, so the inspection procedure requirements must be considered.
Weld Inspection and Industrial Parts
The KEPLER KF-290 can be used for inspecting internal defects in weld seams and metal parts such as detecting discontinuities that may arise from welding processes, manufacturing or machine usage.
For weld inspection, the correct straight probe or angled probe should be selected based on material thickness, part shape, and testing method. It is also necessary to use standard blocks and relevant calibration procedures.
The pass/fail determination must use standards, acceptance criteria, and approved inspection procedures for that work; relying solely on waveform appearance as a criterion should not be done.
Data Connectivity
The device supports RS232 and USB interfaces according to the catalog data for connecting external devices that are compatible. Communication formats, software compatibility, and accessory checks must be performed before actual use.
The catalog specifies support for EPSON Ink-Jet printers but does not confirm all compatible printer models; therefore, verification should be done prior to ordering or designing a reporting system.
Preparation Guidelines and Inspection
- Check the condition of the instrument, probes, signal cables, and batteries before use.
- Select straight or angled probes suitable for material and inspection path.
- Verify the speed of sound in tested materials and set according to procedures.
- Calibrate range and sensitivity with appropriate reference blocks.
- Select Pulse-Echo, Dual or Through Transmission mode as per testing method.
- Adjust Gain, Damping and waveform display according to inspection procedure.
- Prepare the surface of the workpiece and use Couplant appropriately.
- Maintain probe movement along the inspection path with controlled pressure and continuous contact.
- Record positions and characteristics of detected indications as per inspection procedures.
- Evaluate results by referencing relevant standards and acceptance criteria.
Usage Examples and Guidelines
- Inspect weld quality in structural steel work
- Check internal defects in steel plates and metal parts
- Inspect pipe and industrial system welds
- Detect discontinuities within machine components
- Inspect castings and formed parts as appropriate
- Apply for tank inspection and production equipment
- Use for quality control during manufacturing and NDT work
- Check the condition of parts during machinery maintenance
Included Accessories (Included Accessories)
- KEPLER KF-290 Crack Detection Device
- Lithium Battery
- Power Adapter 9V / 3A
- Connector probes LEMO-Q9 and LEMO-Q6 as per catalog list
- Neck Strap
- Wrist Strap
- Hood for the unit
- Straight Probe
- Angle Probe
- Couplant
- Certificate
- Warranty Card
- User Manual (Manual)
Optional Accessories (Optional Accessories)
- RS232 Communication Cable
- USB Communication Cable
- Flash Disk
Considerations
- The KF-290 specifications differ from the KF-500, especially in maximum sound speed range and Dynamic Range
- Select probes and frequencies suitable for material thickness and type of defect to be detected
- UT inspection requires operators with knowledge and skills as per job requirements
- Calibrate and check the performance of the device before starting work according to specified procedures
- The reflected signal display cannot automatically confirm the type or actual size of defects
- Using RS232, USB or printer must verify compatible cables and accessories
- Check the probe types and connectors shipped before ordering
- Do not use IP65 data or advanced functions of KF-320P and KF-860C with KF-290 without documentation confirmation
Write Your Own Review
This website uses cookies
We use cookies to make the site work properly, to understand how it is used, and to show content that is relevant to you. You choose which types to allow; strictly necessary cookies are always on. Privacy Policy
🤖 AI Assistant
Ask about products, specs and replacement models
Hello 👋 Ask us anything — find products, compare specs, or troubleshoot.
🗑 Clear history